1. Project Overview and Application Challenges
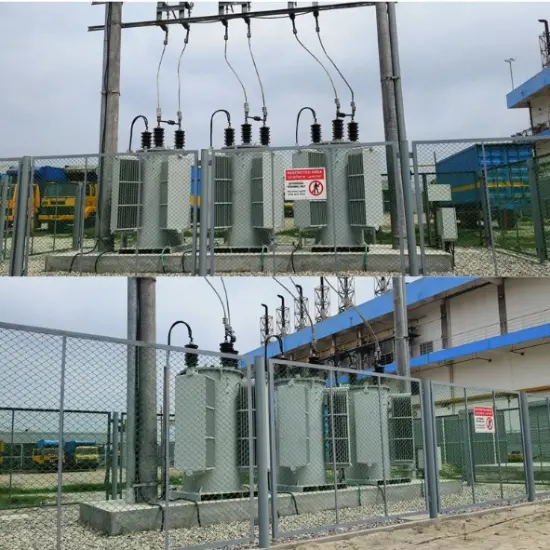
Geographic environment: The project is located in a typical industrial mining environment in South Africa. The local grid infrastructure is relatively aged, and the site is characterized by heavy dust and large diurnal temperature variations, placing stringent demands on the ingress protection and insulation performance of electrical equipment.
Application conditions and load characteristics: As the core power center of the site, this facility carries impact loads from large crushing equipment, conveyor belts, and mine winders. Such loads draw high starting currents and generate significant harmonic content, and the production process is highly continuous — unplanned outages are absolutely not permitted.
Legacy pain points: The existing distribution system was outdated, with low enclosure ingress protection that could not cope with the site's dusty environment. The old switchgear also lacked comprehensive five-prevention interlocking (preventing breaker misoperation, isolator operation under load, earthing switch closure on a live circuit, breaker closure with the earthing switch closed, and entry into an energized compartment), resulting in low operational safety. With capacity expansion underway, a medium-voltage distribution solution with high short-circuit withstand capability, safe and flexible operation, and a high degree of intelligence was urgently required.
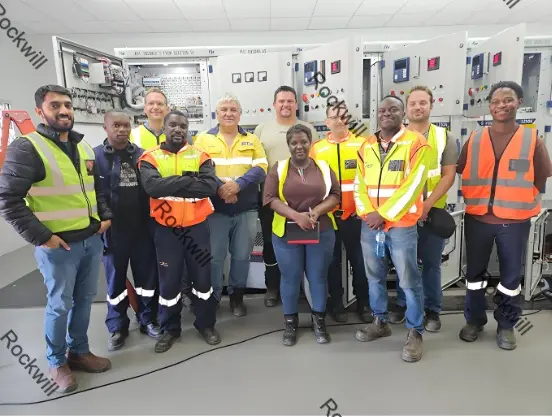
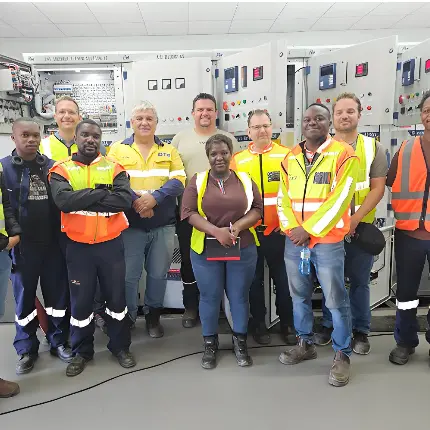
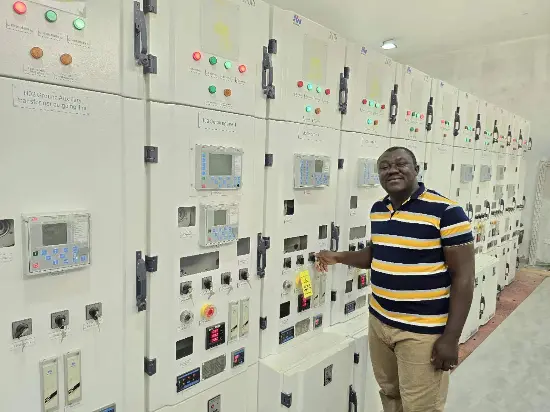
Figure 1: Project team with panoramic view of the distribution room
2. Option Comparison and Selection Basis
Based on South African grid standards (complying with IEC or SANS standards), high reliability requirements, and ease of maintenance, the project conducted a systematic comparison between fixed-type switchgear and KYN28 withdrawable switchgear:
| Comparison Dimension |
Conventional Fixed-Type / Ring Main Unit |
KYN28 Metal-Clad Withdrawable Switchgear (adopted) |
Technical Note |
| Maintenance flexibility |
Breakers are fixed-mounted; maintenance requires long outages and spare parts replacement is complex |
Truck-type design; core modules can be fully withdrawn for rapid replacement using a spare truck, greatly shortening outage time |
Suited to continuous-process industrial and mining enterprises |
| Safety protection |
Relatively simple compartment separation with higher arc fault risk |
Rigorous metal-clad compartmentalization (busbar, breaker, cable, and instrument compartments independent) with comprehensive mechanical and electrical five-prevention interlocking |
Protects the personal safety of O&M personnel |
| Intelligent expansion |
Limited instrument compartment space, unable to accommodate large integrated protection relays |
Ample instrument compartment space, readily accommodating advanced feeder protection relays with event recording and communications |
Meets digital O&M requirements |
| Insulation performance |
Air insulation distances constrained by enclosure dimensions |
High-grade SMC insulation components and composite insulation technology with large specific creepage distance, suited to dusty and humid environments |
Improves operational stability |
| Compatibility |
Compatible only with specific legacy breaker models |
High compatibility; successfully adapted to mainstream vacuum breaker trucks and load-break switch trucks |
Reduces full-lifecycle spare parts cost |
Selection conclusion: Given the rigorous requirements for supply reliability and maintenance efficiency in South African industrial projects, the KYN28 metal-clad withdrawable switchgear — with its flexible interchangeability, exceptionally high safety, and powerful intelligent interfaces — proved the optimal solution for this project.
3. System Configuration and Engineering Implementation
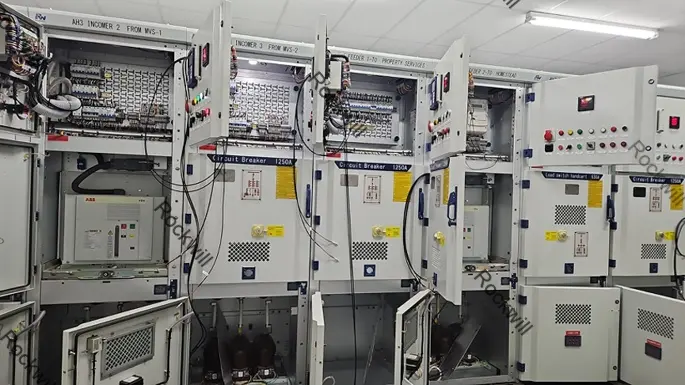
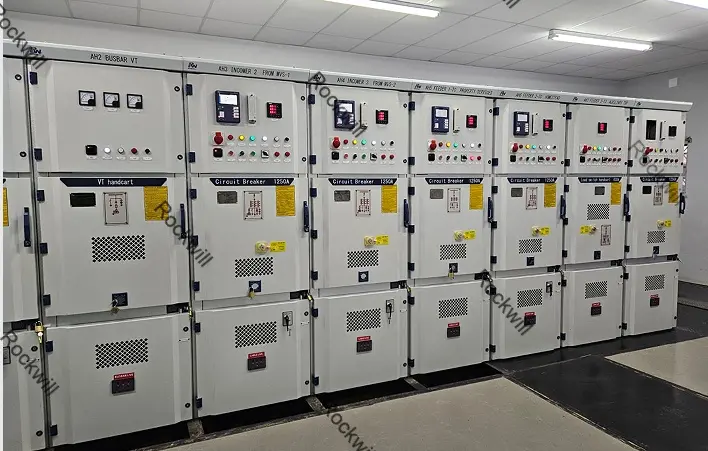
Figure 2: Panoramic internal view of the switchgear in the distribution room
3.1 Switchgear Configuration and Structure
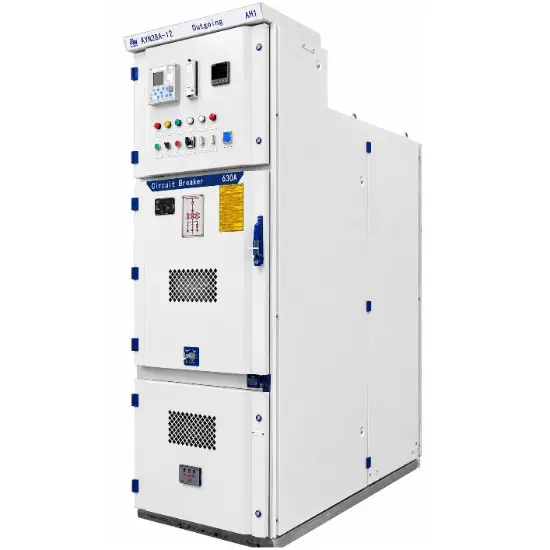
- Configuration: KYN28 series indoor metal-clad withdrawable switchgear was selected. The enclosure is fabricated from aluminum-zinc coated steel sheet, CNC-machined and assembled, offering outstanding corrosion and oxidation resistance.
- Core components: The incoming and feeder cubicles (AH1, AH3, AH4, etc.) are fitted with high-performance vacuum breaker trucks rated at 1250 A, recognized for low chopping current and long electrical life. Notably, cubicle AH6 is equipped with a 630 A load-break switch truck for switching control of specific circuits, demonstrating configuration flexibility.
- Construction points: Enclosure sections are bolted together; busbar bridge connections are torque-tightened and coated with conductive paste to minimize contact resistance.
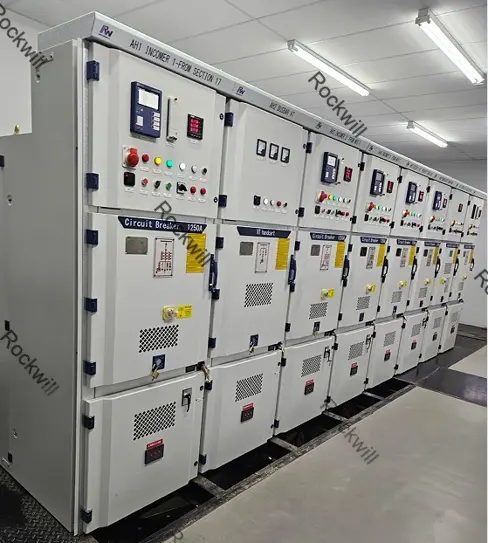
Figure 3: KYN28 switchgear view
3.2 Secondary Protection and Intelligent Monitoring
- Configuration: Critical feeder cubicles are equipped with advanced feeder protection relays.
- Functional highlights: Beyond overcurrent and instantaneous protection, the protection device provides powerful Sequence of Events Recording (SER). As shown in Figure 4, it precisely logs millisecond-level action sequences (such as CB_CLOSE, TRIP, and VOLT_PRES state transitions), delivering black-box-level data support for rapid post-fault root-cause analysis.
- Commissioning process: Secondary injection tests on the protection settings were completed to ensure precise tripping under overload or short-circuit conditions, while data was uploaded to the central control room SCADA system via the communication interface.
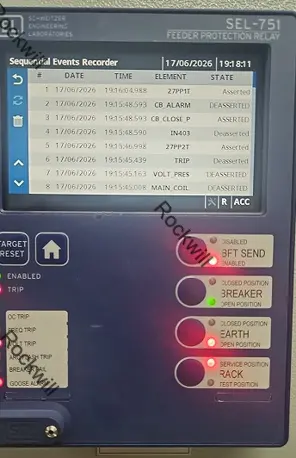
Figure 4: Close-up of the protection device screen
3.3 Electrical Connections and Workmanship Details
- Configuration: Main busbars use high-purity copper bars with clearly color-coded heat-shrink sleeving. The cable compartment offers generous space, facilitating bend radius control for large cross-section cables.
- Construction points: As shown in Figure 5, cable termination workmanship is standardized with clear three-phase separation. Cubicle lighting and heater circuits are wired independently to prevent condensation from affecting insulation.
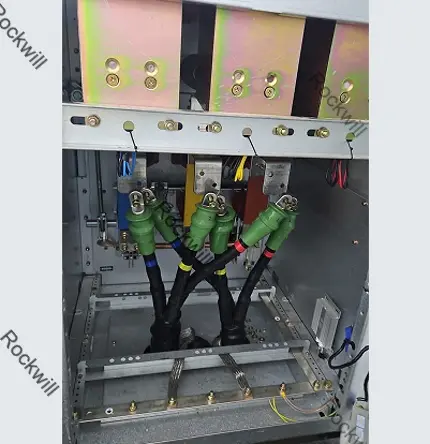
Figure 5: Internal connections in the cable compartment
3.4 Acceptance and Testing
- Test scope: Power frequency withstand voltage tests, main circuit resistance measurement, breaker mechanical characteristic tests (opening and closing times and velocity), and protection trip tests were strictly executed.
- Results: All parameters complied with the IEC 62271 series and the manufacturer's technical specifications. Energization was successful on the first attempt.
- Ease of operation: Since commissioning, the truck racking mechanism has operated smoothly and with ease, and the mechanical interlocking logic is rigorous, eliminating any possibility of misoperation. O&M personnel reported that replacing a spare breaker truck takes only 15 minutes, greatly improving emergency response speed.
- Protection accuracy: The protection devices have operated stably. During an external line transient fault, fault recording was accurately captured, helping the O&M team quickly identify and eliminate the line hazard and preventing an unnecessary upstream trip.
- Environmental adaptability: Despite a certain level of dust on site, thanks to the sound sealing design of the KYN28 and its IP4X or higher ingress protection, internal components remained clean, with no creepage flashover incidents caused by dust accumulation.
- Load capability: During full-load operation, infrared thermography showed normal temperatures at busbar joints and cable terminations, with temperature rise controlled within standard limits.
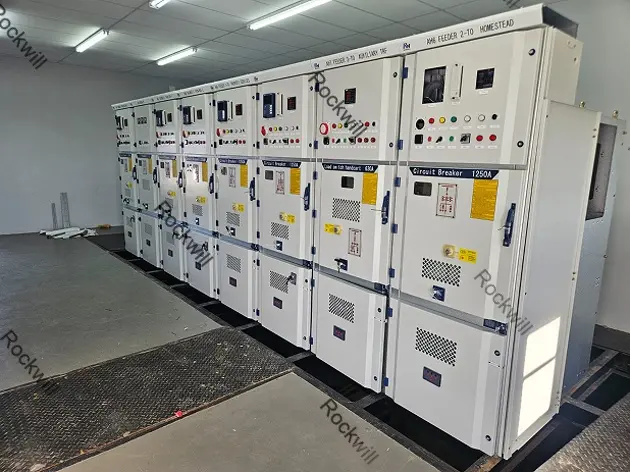
Figure 6: Side view of the distribution room
5. Full Lifecycle Cost Advantage Analysis
Compared with conventional fixed cubicles or low-end ring main units, the high-specification KYN28 solution adopted in this project offers advantages in the following respects:
| Cost Dimension |
Advantage of the High-Specification KYN28 Solution |
| Outage loss cost |
Truck interchangeability shortens fault recovery from hours to minutes. For mining and industrial production, the reduction in lost output is substantial. |
| O&M efficiency cost |
Intelligent relays reduce manual inspection and troubleshooting time; maintenance-free breakers reduce overhaul frequency. |
| Asset life cost |
The metal-clad structure and high-quality materials (aluminum-zinc coated steel sheet, SMC insulation components) give the equipment a service life of over 30 years with high residual value. |
| Safety risk cost |
Comprehensive five-prevention and arc flash protection design minimizes the risk of personal injury and equipment explosion, avoiding potentially enormous liability exposure. |
6. Project Summary and Replication Value
Technical level: This project successfully validated the performance of the "KYN28 cubicle + high-performance vacuum breaker + intelligent protection" combination in a South African heavy-industry environment. It not only resolved supply reliability issues but also improved O&M transparency through digital means.
Economic level: Although the initial equipment investment is somewhat higher than for ordinary switchgear, its extremely low failure rate, very short repair time, and long service life make its Total Cost of Ownership (TCO) highly competitive.
Replication value: This case sets a benchmark for medium-voltage distribution upgrades in mines, cement plants, and chemical plants across South Africa and the wider Southern African region. Particularly in aging grid upgrade projects, this highly compatible and highly safe withdrawable switchgear solution merits broad adoption. When replicating this solution, it is recommended to focus on the local altitude correction factor and industry-specific explosion-proof requirements.
[Practical Summary] Faced with the demanding operating conditions of high dust and heavy impact loads at a South African mining site, "the high ingress protection of the KYN28 cubicle + the rapid fault-recovery capability of truck-type design + the precise traceability of intelligent relay protection" are the three critical elements for safeguarding continuous production. This case demonstrates that in harsh industrial environments, appropriately raising the initial equipment specification level can significantly reduce full-lifecycle O&M risk and cost.

 Login